Blog
Why Air-Operated Diaphragm Pumps Are Ideal for Chemical Processing

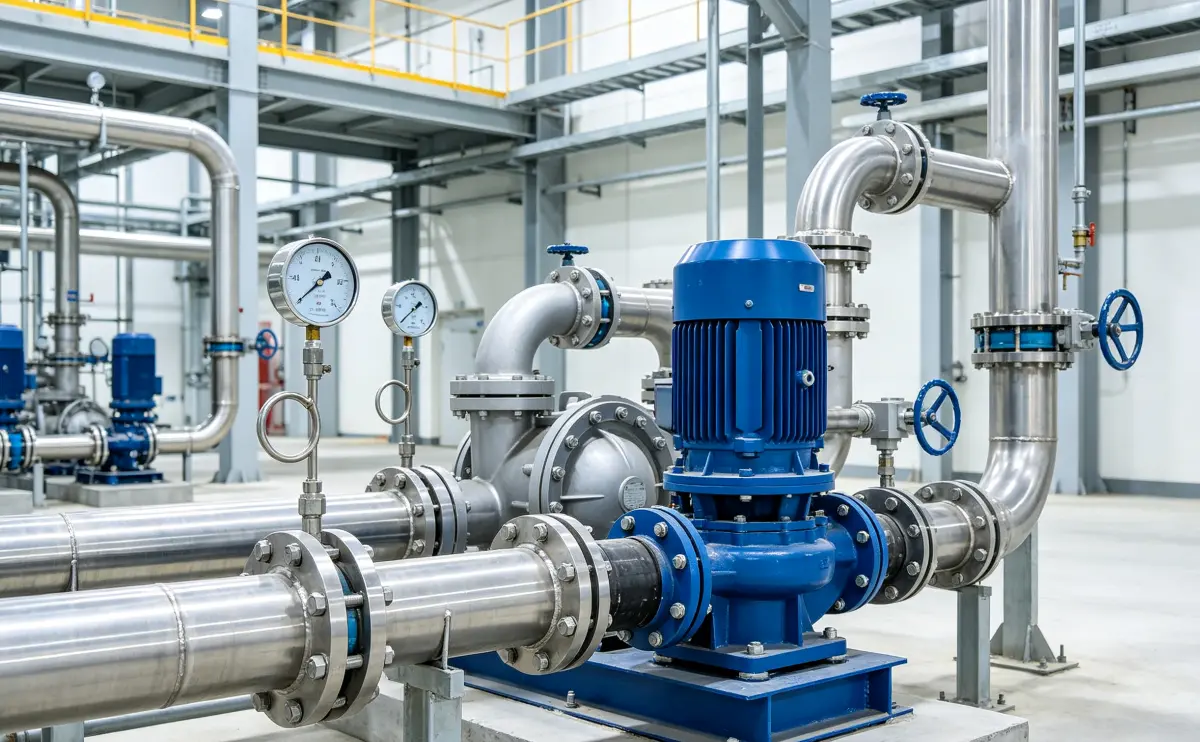
Chemical processing is one of the most demanding environments for any pump. Fluids are often corrosive, toxic, or volatile. Downtime is costly, and safety is non-negotiable. This is where air-operated double diaphragm (AODD) pumps shine.
1. Safety First: No Electricity, No Sparks
AODD pumps run on compressed air—no motors, no electrical components. This makes them inherently safe for flammable and explosive environments, a critical advantage in chemical plants.
2. Excellent Chemical Compatibility
With body options including aluminum, stainless steel, and plastic (PP/PVDF), and diaphragm options including PTFE, Viton, and EPDM, AODD pumps can handle virtually any chemical.
Typical applications:
-
Acid and alkali transfer
-
Solvent dosing
-
Pharmaceutical ingredient handling
-
Wastewater neutralization
3. Self-Priming and Dry-Run Capable
Unlike centrifugal pumps, AODD pumps can run dry without damage and self-prime from a dry state. This simplifies operation and reduces the risk of pump failure.
4. Shear-Sensitive Fluid Handling
AODD pumps use gentle, low-shear pumping action—ideal for emulsions, suspensions, and shear-sensitive chemicals.
5. Easy Maintenance and Low Downtime
Modular design means diaphragms and valves can be replaced quickly, often without removing the pump from the line.
Case Example: Chemical Plant in Southeast Asia
A chemical plant was using centrifugal pumps for acid transfer but faced frequent seal failures and corrosion issues. After switching to a plastic AODD pump with PTFE diaphragms, they reported:
-
60% reduction in maintenance costs
-
Zero leakage incidents
-
18 months of continuous operation without major repair
Considering AODD Pumps for Your Chemical Application?
Our team can help you select the right body and diaphragm materials for your specific fluids. Contact us for a consultation.